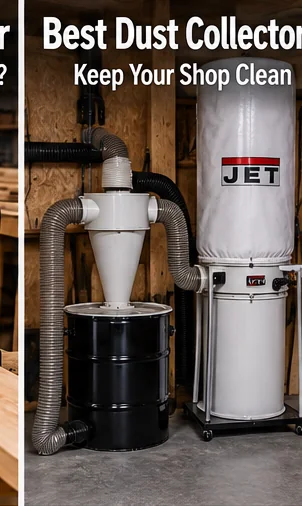
Machines and configurations to compare
1–1.5HP single-stage canister collector
Simple architecture means fewer joints, lower purchase cost and easy mobility.
Best when: your shop is small and you connect one short hose at a time
Watch for: chips hit the collector/filter path directly and can load the filter faster
Cyclone separator + existing collector
A pre-separator can capture most chips before they reach the collector, though every additional fitting and hose run reduces airflow.
Best when: your collector airflow is adequate but filter cleaning/emptying annoys you
Watch for: adds resistance and another container to fit into the shop
2-stage cyclone dust collector
A purpose-built cyclone integrates separation and final filtration and is the cleaner architecture for a serious ducted shop.
Best when: you run several stationary machines through ductwork
Watch for: largest cost, floor/ceiling footprint and installation complexity
Cyclones are primarily separation devices
Air spins so heavier chips and dust fall into a bin before the airstream reaches the filter. That reduces filter loading and makes chip disposal cleaner.
Single-stage systems can still collect very well
With a large canister, short 4-inch hose and clean filter, a single-stage collector can move excellent air at one machine. The cheaper machine is not automatically the weaker choice.
Every separator has a pressure cost
Cyclone bodies, elbows and hoses add resistance. A weak collector with an elaborate separator can move less air at the tool than a simpler short-hose system.
Drum emptying is part of workflow
A transparent bag shows when it is full but can be messy to change. A cyclone drum is easier to wheel away but must be sealed well; leaks can destroy separation and airflow.
Permanent duct pushes the decision toward cyclone
Once the collector lives in one place and serves multiple blast gates, filter maintenance and chip handling become bigger operational issues. That is where integrated two-stage systems make more sense.
Dust collection is about air at the machine, not the catalog CFM number
Collector airflow is only the beginning. Hose diameter, duct length, elbows, flex hose, blast gates, filters and the machine's hood geometry all subtract from the air that reaches the cutter. A system advertised at a huge free-air number can perform poorly at the machine if the duct is undersized or the filter is loaded.
Large chips and fine airborne dust are also different problems. A planer can fill a bag with chips while still releasing fine dust into the room. A table saw often needs collection both below the blade and above the guard. Sanding produces relatively little chip volume but a great deal of fine dust. Design around the machines that are hardest to capture, not the machine with the biggest dust port.
Filtration and separation solve different problems
A cyclone or separator keeps chips out of the filter, preserving airflow and making disposal easier. The final filter controls what small particles return to the room. You want both good separation and fine filtration. A huge collector with a coarse bag can move a lot of air while redistributing fine dust through the shop.
Wood dust is not merely a cleanliness issue. OSHA notes respiratory, skin and other health hazards associated with wood dust, and local exhaust at the point of generation is a primary control. Dust collection should therefore be treated as shop infrastructure rather than an optional accessory.
Before checkout
- Machine fits the room with infeed and outfeed clearance
- Electrical circuit matches voltage and amperage requirements
- Dust port size matches the collection plan
- Guards, riving knife or cutter guards are present and usable
- Replacement blades, knives, inserts or belts are readily available
- Fence/table adjustments lock without visible deflection
- Mobile base or fixed placement is decided before assembly
- Noise and dust strategy are acceptable for the building
- Warranty and freight-return terms are understood
- First accessory budget includes blades/bits, dust adapters and work support
The hidden costs that belong in the machine budget
Cutters and consumables: the included blade, belt, knives or bits are often only a starting point. A premium ripping/crosscut blade, resaw blade, router bit or carbide inserts can materially change the machine. Put that cost in the first-day budget rather than judging the machine forever on the stock consumable.
Work support: long stock needs infeed/outfeed support; sheet goods need a breakdown surface; benchtop machines need a rigid stand or cabinet. Many disappointing machine purchases are really support-system problems.
Dust adapters and hose: machines rarely arrive with exactly the fitting your collector uses. Budget gates, reducers, short flex connections and, where appropriate, above-table or near-cutter pickup.
Electrical and mobility: a 230V circuit, mobile base or dedicated switch can change total installed cost significantly. A machine that blocks the shop when not in use has a real daily cost even if the invoice was cheap.
How to evaluate it in the first week
Before changing the factory setup aggressively, assemble the machine carefully, verify guards, check the table/fence/cutter relationships specified in the manual and make test cuts on known straight stock. Record the baseline. If a cut is wrong, diagnose one variable at a time: blade or cutter condition, fence alignment, table support, feed technique, dust buildup, then machine adjustment. Replacing several settings at once makes it harder to learn what the machine actually needed.
Keep the shipping material until the machine passes inspection. Large stationary tools are expensive to return by freight, and visible shipping damage should be documented before the crate or box disappears. Register the warranty, save the model/serial number and download the current manual; five years later those small administrative steps are surprisingly valuable.
Frequently asked questions
Does a cyclone increase CFM?
No. It adds separation and also adds resistance; the system must have enough fan performance to overcome the additional pressure drop.
Can I add a cyclone to a shop vac?
Yes, small high-pressure separators are common and very effective for chips/dust before a vacuum filter.
Is a cyclone worth it for one planer?
It can be if chip volume is huge and filter/bag emptying is a recurring problem, but a large simple collector may be cheaper.
Which is better for fine dust?
Final filter quality determines what air returns to the shop; separation protects that filter but does not replace it.
Primary references
Affiliate disclosure: WoodShopMachines.com may earn from qualifying purchases through Amazon Associates and eBay Partner Network at no extra cost to you. Product links are shopping paths, not evidence that a larger or more expensive machine is automatically the right choice.